Electro-hydraulic servo press brake
The precision configuration: both cylinders closed-loop synchronised through imported servo proportional valves and Italian grating rulers, with crowning adjusted by the CNC itself. 22 standard models from 30 to 400 ton, seven control systems from entry LCD to 8+1 axes.
What this machine is
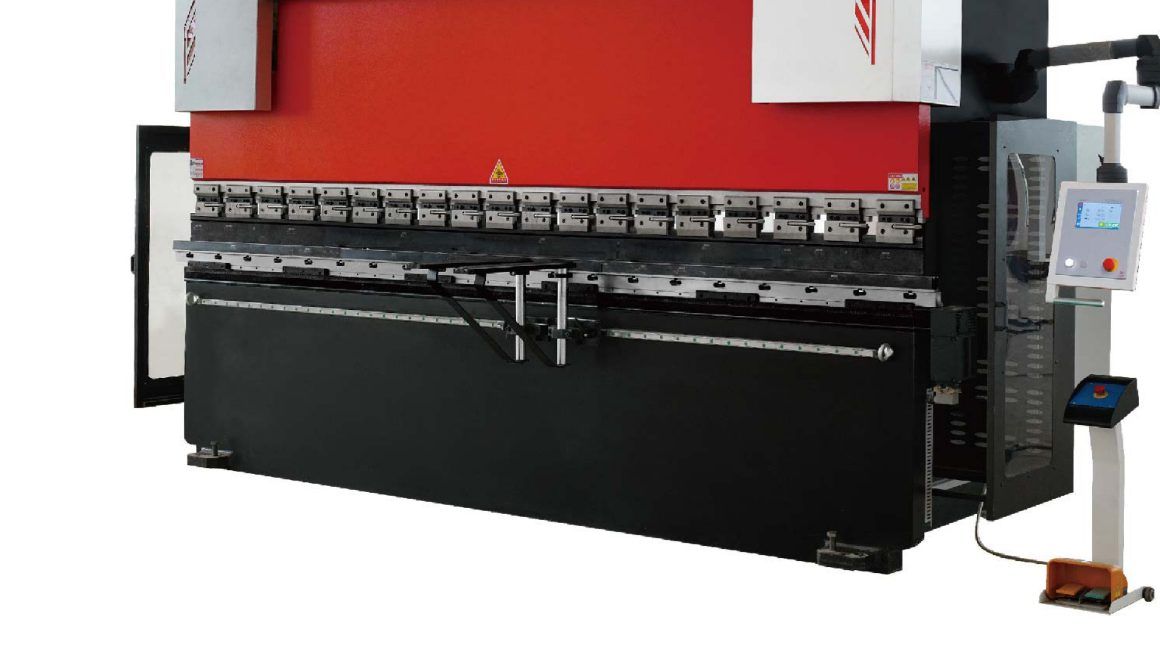
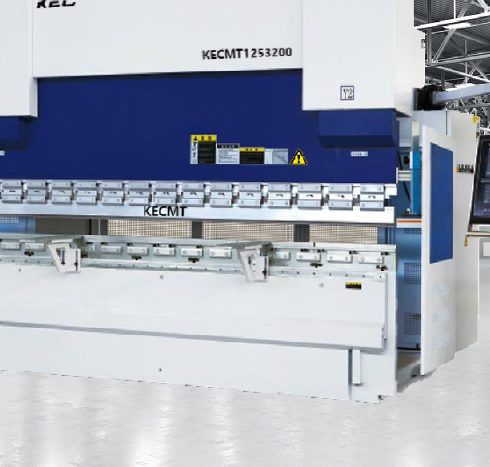
An electro-hydraulic press brake replaces the mechanical link between the two cylinders with a closed loop. Both main cylinders are synchronised by imported German electro-hydraulic servo proportional valves working against Italian GIVI grating rulers: exact position feedback from each end of the ram, corrected against the other in real time, so bending accuracy and ram repeat positioning stay tight through the stroke.
We build these in 22 standard models from WE67K-30/1600 to WE67K-400/4000 — 30 to 400 ton nominal pressure across bending lengths from 1.6 to 6 m — with a choice of seven control systems, from a 128 x 64 industrial LCD up to a 21.5-inch touch screen driving 8+1 axes. Special models with non-standard throat depth and open height are custom-built to order.
Specifications
| No. | Model | Nominal pressure (kN) | Table length (mm) | Between housings (mm) | Throat depth (mm) | Stroke / strokes (mm / spm) | Open height (mm) | Main motor (kW) | Backgauge travel (mm) | Overall LxWxH (mm) |
|---|---|---|---|---|---|---|---|---|---|---|
| 1 | WE67K-30/1600 | 300 | 1600 | 1000 | 250 | 150 / 15 | 280 | 4 | 400 | 2000 x 1500 x 2100 |
| 2 | WE67K-45/2000 | 450 | 2000 | 1675 | 250 | 160 / 15 | 380 | 5.5 | 500 | 2400 x 1600 x 2200 |
| 3 | WE67K-70/2500 | 700 | 2500 | 2095 | 250 | 160 / 12 | 400 | 5.5 | 500 | 2700 x 1700 x 2300 |
| 4 | WE67K-70/3200 | 700 | 3200 | 2570 | 250 | 160 / 12 | 400 | 5.5 | 600 | 3400 x 1800 x 2300 |
| 5 | WE67K-90/2500 | 900 | 2500 | 2095 | 320 | 180 / 12 | 420 | 7.5 | 600 | 2800 x 1900 x 2400 |
| 6 | WE67K-90/3200 | 900 | 3200 | 2600 | 320 | 180 / 10 | 420 | 7.5 | 800 | 3600 x 1900 x 2400 |
| 7 | WE67K-110/3200 | 1100 | 3200 | 2600 | 320 | 200 / 10 | 450 | 7.5 | 600 | 3400 x 1800 x 2500 |
| 8 | WE67K-110/4000 | 1100 | 4000 | 3100 | 320 | 200 / 10 | 450 | 7.5 | 800 | 4200 x 1900 x 2500 |
| 9 | WE67K-130/3200 | 1300 | 3200 | 2550 | 320 | 200 / 10 | 450 | 7.5 | 600 | 3350 x 2000 x 2550 |
| 10 | WE67K-130/4000 | 1300 | 4000 | 3450 | 320 | 200 / 8 | 450 | 7.5 | 800 | 4100 x 2100 x 2600 |
| 11 | WE67K-160/3200 | 1600 | 3200 | 2540 | 320 | 220 / 8 | 500 | 11 | 600 | 3400 x 1900 x 2700 |
| 12 | WE67K-170/4000 | 1700 | 4000 | 3140 | 320 | 220 / 8 | 500 | 11 | 800 | 4200 x 2200 x 2700 |
| 13 | WE67K-170/6000 | 1700 | 6000 | 4740 | 320 | 220 / 6 | 500 | 11 | 1000 | 6200 x 2200 x 2700 |
| 14 | WE67K-200/3200 | 2000 | 3200 | 2540 | 320 | 260 / 6 | 580 | 11 | 800 | 3400 x 2300 x 2900 |
| 15 | WE67K-200/4000 | 2000 | 4000 | 3140 | 320 | 260 / 6 | 580 | 15 | 800 | 4200 x 2300 x 3000 |
| 16 | WE67K-200/5000 | 2000 | 5000 | 3940 | 320 | 260 / 5 | 580 | 15 | 1000 | 5200 x 2300 x 3100 |
| 17 | WE67K-250/4000 | 2500 | 4000 | 3120 | 400 | 280 / 5 | 620 | 18.5 | 800 | 4200 x 2400 x 3600 |
| 18 | WE67K-250/5000 | 2500 | 5000 | 3920 | 400 | 280 / 5 | 620 | 18.5 | 1000 | 5200 x 2400 x 3600 |
| 19 | WE67K-250/6000 | 2500 | 6000 | 4720 | 400 | 280 / 4 | 620 | 18.5 | 1000 | 6200 x 2400 x 3600 |
| 20 | WE67K-300/5000 | 3000 | 5000 | 3910 | 400 | 300 / 4 | 650 | 22 | 1000 | 5200 x 2800 x 4100 |
| 21 | WE67K-300/6000 | 3000 | 6000 | 4710 | 400 | 300 / 3 | 650 | 22 | 1200 | 6200 x 2800 x 4100 |
| 22 | WE67K-400/4000 | 4000 | 4000 | 3100 | 400 | 320 / 3 | 700 | 30 | 1000 | 4200 x 2900 x 3900 |
Specifications per the factory catalogue. The above are standard machine models; throat depth and open height can be customized to different production requirements.
Reading the model table
The model number reads as tonnage x bending length — a WE67K-160/3200 bends 160-ton work across a 3.2 m bed. The electro-hydraulic range runs longer strokes and taller open heights than the mechanically synced range at the same tonnage: 150–320 mm stroke and 280–700 mm open height against 100–220 mm and 240–560 mm. That extra daylight is what lets you stand deep tooling and tall boxes in the machine.
Machine structure
What separates this range from the standard machine:
- Frame. Split steel plates, welded and then stress-relieved in a large tempering furnace to remove welding and machining stresses — the same foundation both ranges stand on.
- Servo drive with on-demand oil supply. The main motor can be a high-performance servo motor running a fully closed-loop electro-hydraulic servo system. Pressure and flow signals from the CNC go to the driver's analog input; pressure and speed sensors track flow and pressure changes in real time and feed monitoring signals back for immediate correction — a closed-loop method with no overflow. The results are lower energy use, lower oil temperature and higher efficiency.
- Cylinder synchronisation. Both main cylinders run closed-loop against each other through imported German electro-hydraulic servo proportional valves and Italian GIVI grating rulers — precise feedback, accurate ram motion, and bending and repeat-positioning accuracy well beyond what a mechanical link can hold.
- V-axis crowning compensation. Compensates for ram deflection during bending so long sheets keep a consistent angle. The compensation amount is adjusted automatically by the CNC system — no hand adjustment between jobs.
- C-plate mounted grating rulers. High-precision grating rulers are mounted on C-shaped plates at both sides of the frame, so frame deformation during bending does not reach the measurement — the accuracy you program is the accuracy the ram keeps.
- Cylinders and hydraulics. Cylinders machined by specialist manufacturers, with a fully imported German Rexroth valve group, imported sealing rings and German pipe fittings — high-speed, stable, leak-free operation.
- Backgauge. The X-axis backgauge is built from left and right guide rail seats, crossbeam, adjusting seats, brackets, adjustable supports, base plates, adjusting lead screws and gauge fingers, driven front-to-back by a dedicated X-axis servo motor. The R-axis backgauge adds a servo motor and reducer, moving the crossbeam up and down along linear guides through gear and rack.
- Electrics. Main electrical components are Schneider or other established imported and joint-venture brands.
Control systems
Seven control options cover everything from a basic NC-style station to a full 8+1 axis production cell. All run on 24 V DC ±20%, operate from 0–50 °C and carry IP54 protection.
| System | Display | Axes | Highlights |
|---|---|---|---|
| DA66S (imported) | 24 in, 1920 x 1080 | 6+1 (Y1+Y2+X+R+Z1+Z2+V) | 2D full graphical programming with 3D real-time machine simulation; fully automatic bending sequence calculation with collision warning; nanometer position sampling; Modusys modular axis expansion; multi-station tooling visualisation; one-click DXF import; embedded Linux; Industry 4.0 networking, offline programming and remote diagnosis |
| DA69S (imported) | 21.5 in, 1920 x 1080 multi-touch | 8+1 (Y1+Y2+X1+X2+R1+R2+Z1+Z2+V) | High-precision dual-cylinder closed-loop sync; automatic hydraulic crowning control; real-time display of actual vs programmed position on every axis; bending count and batch production management; 2D/3D graphical programming with collision detection; ergonomic pendant; DXF import |
| DA53TX (imported) | 10.1 in, 1366 x 768 | — | Dual-cylinder Y1/Y2 closed-loop sync; X+R backgauge linkage; crowning compensation; automatic bending sequence calculation and programming; process library; 100 program steps; panel or pendant mount |
| CT15 (imported) | 15 in, 1024 x 768 | 6+1 | Dual-cylinder closed-loop sync; automatic crowning; real-time position display; 2D graphical programming with 1000+ program steps; panel or pendant mount; controls servo, variable-frequency and two-speed AC motors |
| CT12 (imported) | 128 x 64 industrial LCD | 4+1 (Y1+Y2+X+R+V) | Dual-cylinder high-precision closed-loop sync; full closed-loop control of ram stroke and bending pressure; 100 program steps; industrial-grade anti-interference design; servo, variable-frequency and two-speed AC motor control |
| DE530 (domestic) | 10.1 in, 1366 x 768 | 6+1 | Dual-cylinder closed-loop sync; automatic crowning; 2D graphical programming with automatic sequence calculation; bending count and batch production management; process, tool and material libraries; USB data transfer |
| DE15 (domestic) | 128 x 64 industrial LCD | 4+1 | Dual-cylinder high-precision closed-loop sync; full closed-loop control of ram stroke and bending pressure; 100 program steps; industrial-grade anti-interference design; servo, variable-frequency and two-speed AC motor control |
Main configuration
| Item | Component | Brand / note |
|---|---|---|
| 1 | Main motor / main servo motor (optional) | Siemens / ESTUN (China) |
| 2 | Electrical components | Schneider (France) |
| 3 | X, R, Z axis servo motors | Estun / INOVANCE (China) |
| 4 | Servo drives | Estun (China) |
| 5 | Hydraulic valve | Bosch Rexroth |
| 6 | Hydraulic pump | SUNNY (USA) |
| 7 | Oil cylinder | YUKEN |
| 8 | Pipe connectors | EMB |
| 9 | Grating ruler | GIVI (Italy) |
| 10 | Crowning table | CHNVIKEN |
| 11 | Punch and die tooling | CHNVIKEN |
| 12 | Quick clamp (optional hydraulic) | CHNVIKEN / Vila |
| 13 | Laser protection | DSP (Italy) / LNTECH (China) — optional |
| 14 | Rear light curtain protection | KELI / LNTECH |
Installation, training and after-sales
- Foundation. We provide the foundation drawing; you are responsible for the construction work.
- Shipment notice. When the machine is assembled at our works, we notify you of the shipment schedule and what to prepare for installation.
- Installation and commissioning. Our engineers install and commission the machine at your site, with your cooperation — you provide lifting equipment, water, electricity, hydraulic oil and the necessary conditions.
- Training. During installation and commissioning we train your technical staff free of charge and provide technical consultation. If you need an engineer to travel for debugging, that cost is reimbursed at actuals.
- Acceptance. On completion, both parties inspect and accept the machine jointly against the signed technical agreement and its attachments.
- Warranty. Three-guarantee policy from the date of sale, with a three-year quality guarantee from the date of acceptance. Within the warranty period, component damage not caused by the user is replaced free of charge; wearing parts are excluded. After the guarantee expires, lifetime service continues with parts charged at cost.
Related
- CNC torsion bar press brake — the mechanically synced range, same 22-model envelope, TP10S control
- CNC hydraulic press brake — the full range overview and how we configure machines
- Small tonnage press brakes — 220V single-phase machines for small shops
- How much tonnage do you need? — the sizing logic behind the table
- Machine selector tool — answer a few questions and get a recommended configuration
Ask about the electro-hydraulic servo press brake
Send the part you need to bend and we will come back with a configuration and a quote.